Machines
XZ-988 Rotary Shoe Injection Molding Machine
Model: XZ-988/16-20-24-S(C)
Manufactured by Ruian Xingzhong Industrial Co., Ltd., the XZ-988 S(C) is a rotary direct injection shoe machine for PVC/TPR soles molded directly onto uppers. Applications include canvas shoes and casual footwear, subject to matching the upper, last, mould and material formulation.
S(C) uses operator-controlled mould opening and closing; AS(C) automates those mould movements. Both configurations still require material preparation, upper loading and positioning, footwear removal and inspection.
Compare AS(C) automatic mould operation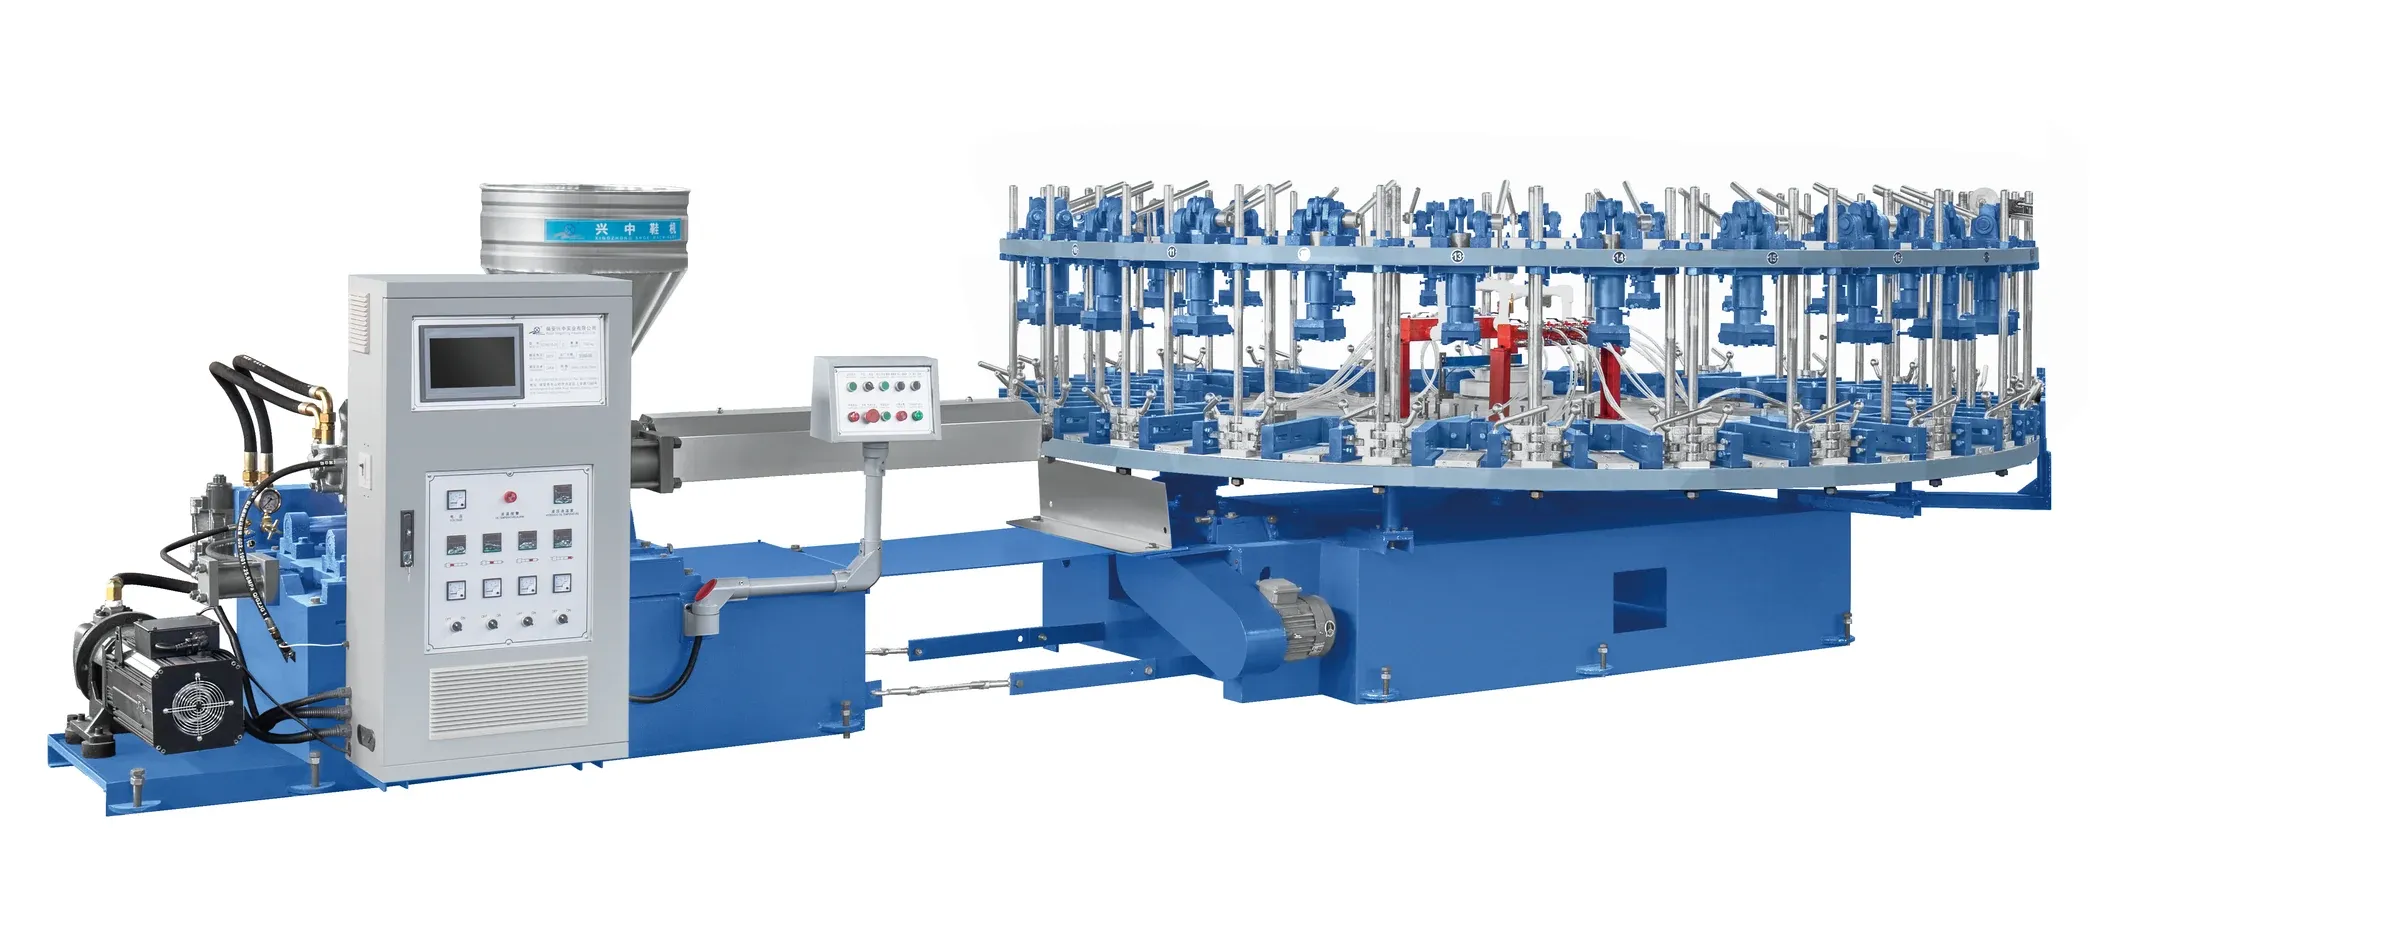
Key Features
Computer-Controlled Operation
The listed configuration includes Siemens control computer and Autonics (Korea) rotary encoder. Review the control configuration with our team to confirm available process settings, status displays and alarms for your application.
View the control configurationPVC & TPR Processing
Designed for PVC and TPR footwear applications, with foamed or non-foamed processing reviewed against the chosen formulation and mould. Confirm the material, required sole properties and footwear design before selecting a production setup.
Explore PVC material optionsMold Cooling System
Chiller-connected aluminum cooling plates help lower mould temperature, improve PVC sole shape retention and reduce cooling-related bulges. Shorter cooling time can support higher output. Xingzhong reports an average output increase of approximately 20% in practical applications, depending on sole thickness, size and production conditions.
Explore the mold cooling systemSimplified Daily Operation
Organize daily work around material preparation, upper loading and positioning, product removal and inspection. Operator allocation and training depend on the footwear and production layout; review these tasks alongside the machine-controlled stages.
Follow the production workflowRotary Production Capacity
Published reference output — 20 station: 300-400 pairs/hour; 24 station: 300-400 pairs/hour. Actual output depends on material formulation, footwear design, moulds, cooling requirements and operator coordination. Reference output is not a guaranteed production rate.
Compare technical specifications
How the XZ-988 Production Process Works
A production overview for direct-injection footwear. Confirm the detailed operating sequence and manual tasks for your S(C) configuration during the project review.
Material Preparation
Prepare the approved PVC or TPR formulation and set the process parameters for the intended footwear. Confirm any material preparation requirements with the supplier.
Explore PVC material optionsUpper Loading & Positioning
The operator loads the upper onto the last and checks its position and fit before moulding. The upper, last and mould must match the intended shoe design.
Review DIP shoe mouldsMould Closing & Indexing
On S(C), the operator controls mould closing before the rotary station is positioned for injection. Follow the machine's operating procedure for the sequence and safety checks; AS(C) provides automatic mould closing.
Review the machine configurationInjection & Sole Formation
The prepared material is plasticized and injected into the mould to form the sole against the upper. Material compatibility and process settings must be checked for the intended bond and shape.
Compare technical specificationsCooling During Rotation
Allow the moulded sole to cool as the rotary production sequence continues. Cooling requirements depend on the material, sole geometry and mould setup.
Compare technical specificationsDemoulding & Inspection
Remove the shoe when it is ready for demoulding, then check appearance, sole formation and the upper-to-sole bond before downstream finishing. Plan these operator tasks as part of the production line.
Discuss your production requirements
Machine data
Technical specifications
Compare all listed configurations below. On smaller screens, scroll the tables horizontally.
20 station
| Specification | Value | Unit |
|---|---|---|
| Station configuration | 20 | stations |
| Injecting screw diameter | 75 | mm |
| Maximum injection capacity | 800 | cm3/shot |
| Screw rotary speed | 200 | RPM |
| Injection pressure | 5-10 | MPa |
| Maximum injection speed | 12 | cm/sec |
| Maximum injection stroke | 180 | mm |
| Productivity per hour | 300-400 | pairs/hour |
| Mould dimension | 340 x 180 x 60 | mm |
| Total power | 50 | kW |
| Machine dimension | 6000 x 3000 x 1800 | mm |
| Machine weight | 6500 | kg |
| Oil capacity | 300 | L |
24 station
| Specification | Value | Unit |
|---|---|---|
| Station configuration | 24 | stations |
| Injecting screw diameter | 75 | mm |
| Maximum injection capacity | 800 | cm3/shot |
| Screw rotary speed | 200 | RPM |
| Injection pressure | 5-10 | MPa |
| Maximum injection speed | 12 | cm/sec |
| Maximum injection stroke | 180 | mm |
| Productivity per hour | 300-400 | pairs/hour |
| Mould dimension | 340 x 180 x 60 | mm |
| Total power | 50 | kW |
| Machine dimension | 6600 x 3600 x 1800 | mm |
| Machine weight | 8500 | kg |
| Oil capacity | 300 | L |
Actual output depends on material formulation, footwear design, moulds, cooling requirements and operator coordination. Reference output is not a guaranteed production rate.
The 20- and 24-station configurations currently share the same published reference output range.
Machine configuration
| Item | Brand | Specification |
|---|---|---|
| Control computer | Siemens | - |
| Rotary encoder | Autonics (Korea) | - |
| Servo motor | INVT | - |
| Gear pump | Chongqing Yedong | 80 |
| Servo driver | INVT | - |
| Rotary unit motor | Haining Yongfa | 2.2 kW |
| Hydraulic valve | Seven ocean (Taiwan) | - |
| Switching power supply | Mean Well (Taiwan) | - |
| Low-voltage electrical components | Schneider / CHNT | - |
| Seals | Hallite (UK) / DINGZING (Taiwan) | Combined seal / U-ring |
| Feeding hydraulic motor | Ningbo Yining | 700 |
| Heating ring / screw cover | Domestic | Ceramic heating ring with insulated screw cover |
| Injection stroke cylinder | In-house | Cylinder diameter 120 mm |
| Rotary table | Domestic | Double-layer |
| Mould holder | Domestic | Scissor type |
| Gear reducer | Domestic | 155 |
| Screw | Zhoushan | 75 mm diameter |
| Automatic rotary table lubrication system | Domestic | PLC controlled |
| Water chiller | Domestic | 5 HP |
The above data is for reference only. Any changes due to actual design requirements will not be notified separately.
Applications
PVC and TPR foaming material
Sport shoes
Casual shoes
Safety shoes
Frequently Asked Questions
What materials can the XZ-988 process?
The machine is intended for PVC and TPR footwear production. Foamed and non-foamed applications require a suitable formulation, mould and process setup. Other materials need a separate compatibility review; the linked material page covers PVC options.
Explore PVC material optionsWhat footwear can this machine produce?
Applications include sports shoes, casual shoes and safety-shoe production, subject to the upper, last, mould and material combination. Share a sample or drawing so we can assess the intended construction. Machine suitability alone does not establish finished-footwear certification.
Review DIP shoe mouldsWhat is the production capacity?
Published reference output — 20 station: 300-400 pairs/hour; 24 station: 300-400 pairs/hour. Actual output depends on material formulation, footwear design, moulds, cooling requirements and operator coordination. Reference output is not a guaranteed production rate. Share your shoe style and target output for a production review.
Compare technical specificationsHow do I choose between 20 and 24 stations?
Compare the available configurations against cooling requirements, product mix, mould investment and factory space. More stations do not automatically mean a proportional increase in hourly output. Use the configuration-specific dimensions and reference output in the table when planning the layout. The 20- and 24-station configurations currently share the same published reference output range.
Compare technical specificationsHow many operators are required?
Staffing is assessed for your shoe style, loading and unloading tasks, shift plan and production layout. Clarify whether material handling, trimming and quality inspection are included in the headcount. Operator training and safe operating procedures are required; no fixed staffing or training-time claim is made here.
Review the operator tasksWhat utilities and installation space are required?
Check the selected configuration's power and machine dimensions in the specifications. Installed power is not a measurement of actual electricity consumption. Allow additional space for access, material handling and maintenance; confirm the electrical supply and cooling or other utility connections in the project proposal.
Compare technical specificationsCan my existing moulds be used?
Existing moulds need a compatibility review covering dimensions, mounting interfaces, lasts and injection position. Matching external dimensions alone is insufficient. Send mould drawings or photographs and details of the intended footwear before assuming compatibility.
Review DIP shoe mouldsWhat should I provide to request a quotation?
Send shoe samples or photographs, material details, the size range, target output, existing mould information, available electrical supply and delivery destination. These details help define the machine, mould and material proposal.
Discuss your production requirements
Export inquiry
Share your requirements of Machine& Mould& Material
We will review your drawings, productivity, quantity and shipping needs before offering integrated solution.